 Availability to be confirmed
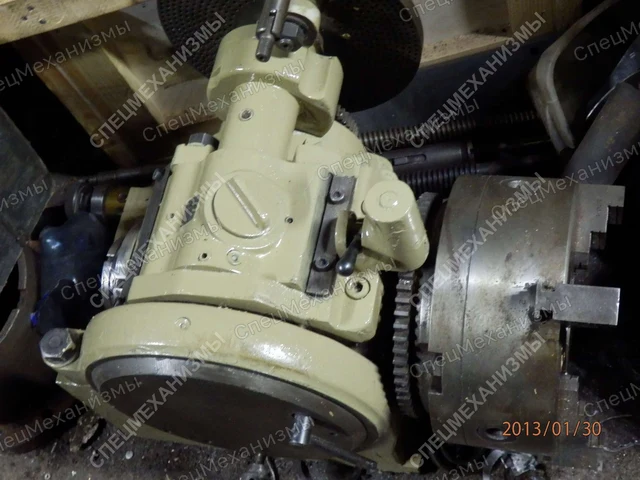
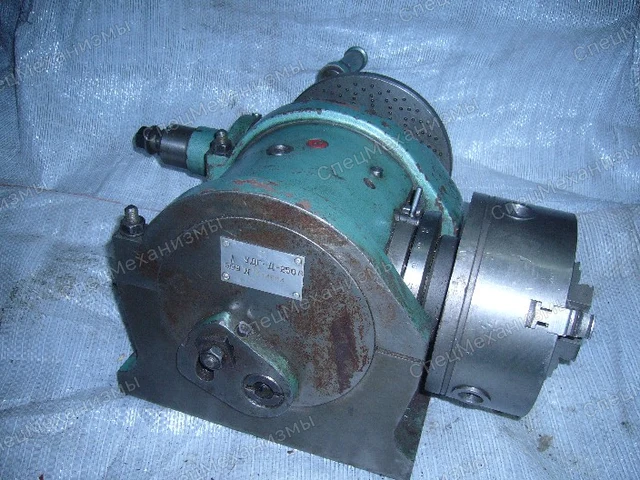
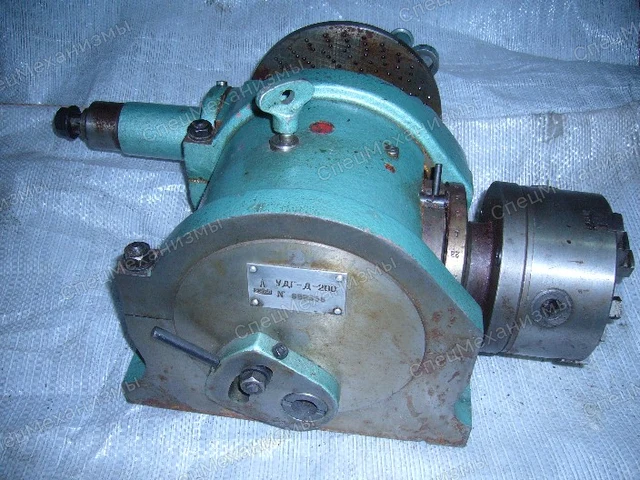
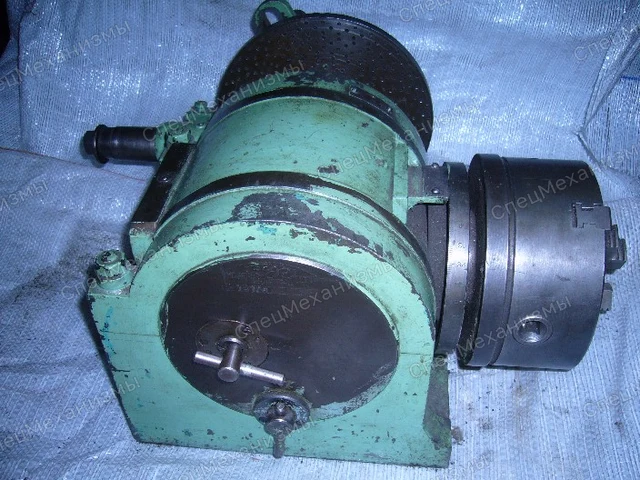
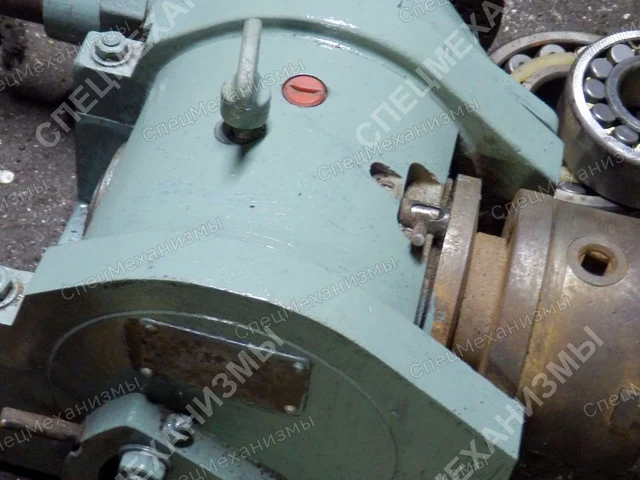
GAMBIN universal dividing head (France)
Dividing heads
- Specifications
- GAMBIN (France)
- Maximum workpiece diameter, mm
- 300
- 3-jaw chuck diameter, mm
- 200
Results: 33
Availability to be confirmed
Dividing heads
 Availability to be confirmed
 Availability to be confirmed
 Availability to be confirmed
 Availability to be confirmed
 Availability to be confirmed
 Availability to be confirmed
 Availability to be confirmed
Tooling for boring machines
 Availability to be confirmed
Tooling — fixtures for securing workpieces on machines, transporting parts and performing assembly operations.
Production tooling, or as it is often called Machine tooling - A type of tooling designed to secure and correctly position a workpiece on the machine for subsequent machining. It is used at various production stages requiring rigid clamping of parts and assemblies: metal cutting, inspection and assembly.
Machine fixtures locate and secure workpieces on metal-cutting machines. Machine tooling consists of special devices used to mount cutting tools and specialised fixtures on metalworking machines. Tooling also substantially extends equipment capabilities and increases productivity.
Machine tooling and fixtures are essential structures required to perform a particular manufacturing operation.
Machine tool fixtures are divided into 6 groups according to their degree of specialisation:
Machine tooling is divided into 4 groups by purpose:
Machine tooling and fixtures are divided into manual, mechanised and automated groups. These devices improve workpiece machining accuracy and increase productivity by speeding up manufacturing operations. Machine fixtures also extend the capabilities of metalworking equipment.
Mechanical engineering uses a wide variety of tooling, including fixtures, auxiliary tools, cutting tools and measuring instruments. Fixtures are additional devices used for machining, assembly and inspection of parts, assemblies and products. By purpose, fixtures are divided into the following types:
By operating characteristics, machine fixtures are classified as universal, for machining various workpieces (machine vices, chucks, dividing heads, rotary tables and similar fixtures); dedicated, for machining a particular workpiece type using interchangeable devices (special vice jaws, shaped chuck jaws and similar components); and special-purpose, for performing specific machining operations on a particular part. Universal fixtures are used in one-off and small-batch production, while dedicated and special-purpose fixtures are used in high-volume and mass production.
Universal modular fixtures are assembled from prefabricated standard elements, parts and assemblies manufactured to high precision. They are used as temporary special-purpose fixtures for a specific operation, after which they are dismantled and their components reused repeatedly in new arrangements and combinations. Further development involves creating units, blocks, individual special parts and assemblies that enable the assembly of temporary special-purpose, dedicated and universal adjustable fixtures.
Assembled and disassembled fixtures (СРП) are also built from standard components, but these are less precise and permit local modifications at mating surfaces. They are used as dedicated fixtures for long-term use. After disassembly, the components can be used to create new arrangements.
Non-dismantlable special-purpose fixtures are assembled from standard general-purpose parts and assemblies as permanent fixtures for long-term use. Their structural components are generally used until fully worn out and are not reused.
A fixture can also be built from two main parts: a standardised base (УБ) and an interchangeable setup (СИ). This design makes a dedicated setup fixture (НСП) adaptable to changes in workpiece design and machining processes. In such cases, only the interchangeable setup is replaced.
General-purpose universal fixtures requiring no setup (УБП) are most common in batch production. They are used to hold rolled-section workpieces and individual blanks. They consist of universal adjustable bodies with permanent, non-removable locating elements, such as chucks and vices, supplied with the machine.
Specialised setup fixtures (СНП) are used for machining parts grouped by design features and locating schemes. Their modular arrangement comprises a basic body structure with interchangeable setups for groups of parts.
Universal adjustable fixtures, like dedicated adjustable fixtures, have fixed bodies and interchangeable parts. However, each interchangeable part is suitable for only one operation on one particular part. When changing operations, universal adjustable fixtures are fitted with new interchangeable setups.
Modular powered clamping systems consist of universal power devices built as separate units. Combined with fixtures, they enable mechanisation and automation of workpiece clamping.
The choice of fixture design largely depends on the type of production. Batch production uses relatively simple fixtures, mainly to achieve the specified workpiece machining accuracy. Mass production also demands high productivity from fixtures, making their designs more complex and requiring quick-action clamps. Even the most expensive fixtures can be economically justified in mass production.
Fixtures consist of the following elements:
Include the model, task, city and country. Attach photos and documents in your email or messaging app.
Include the model, task, city and country. Attach photos and documents in your email or messaging app.